Our Products > Shell & Tube Heat Exchangers
Proven heat transfer, engineered around your process.
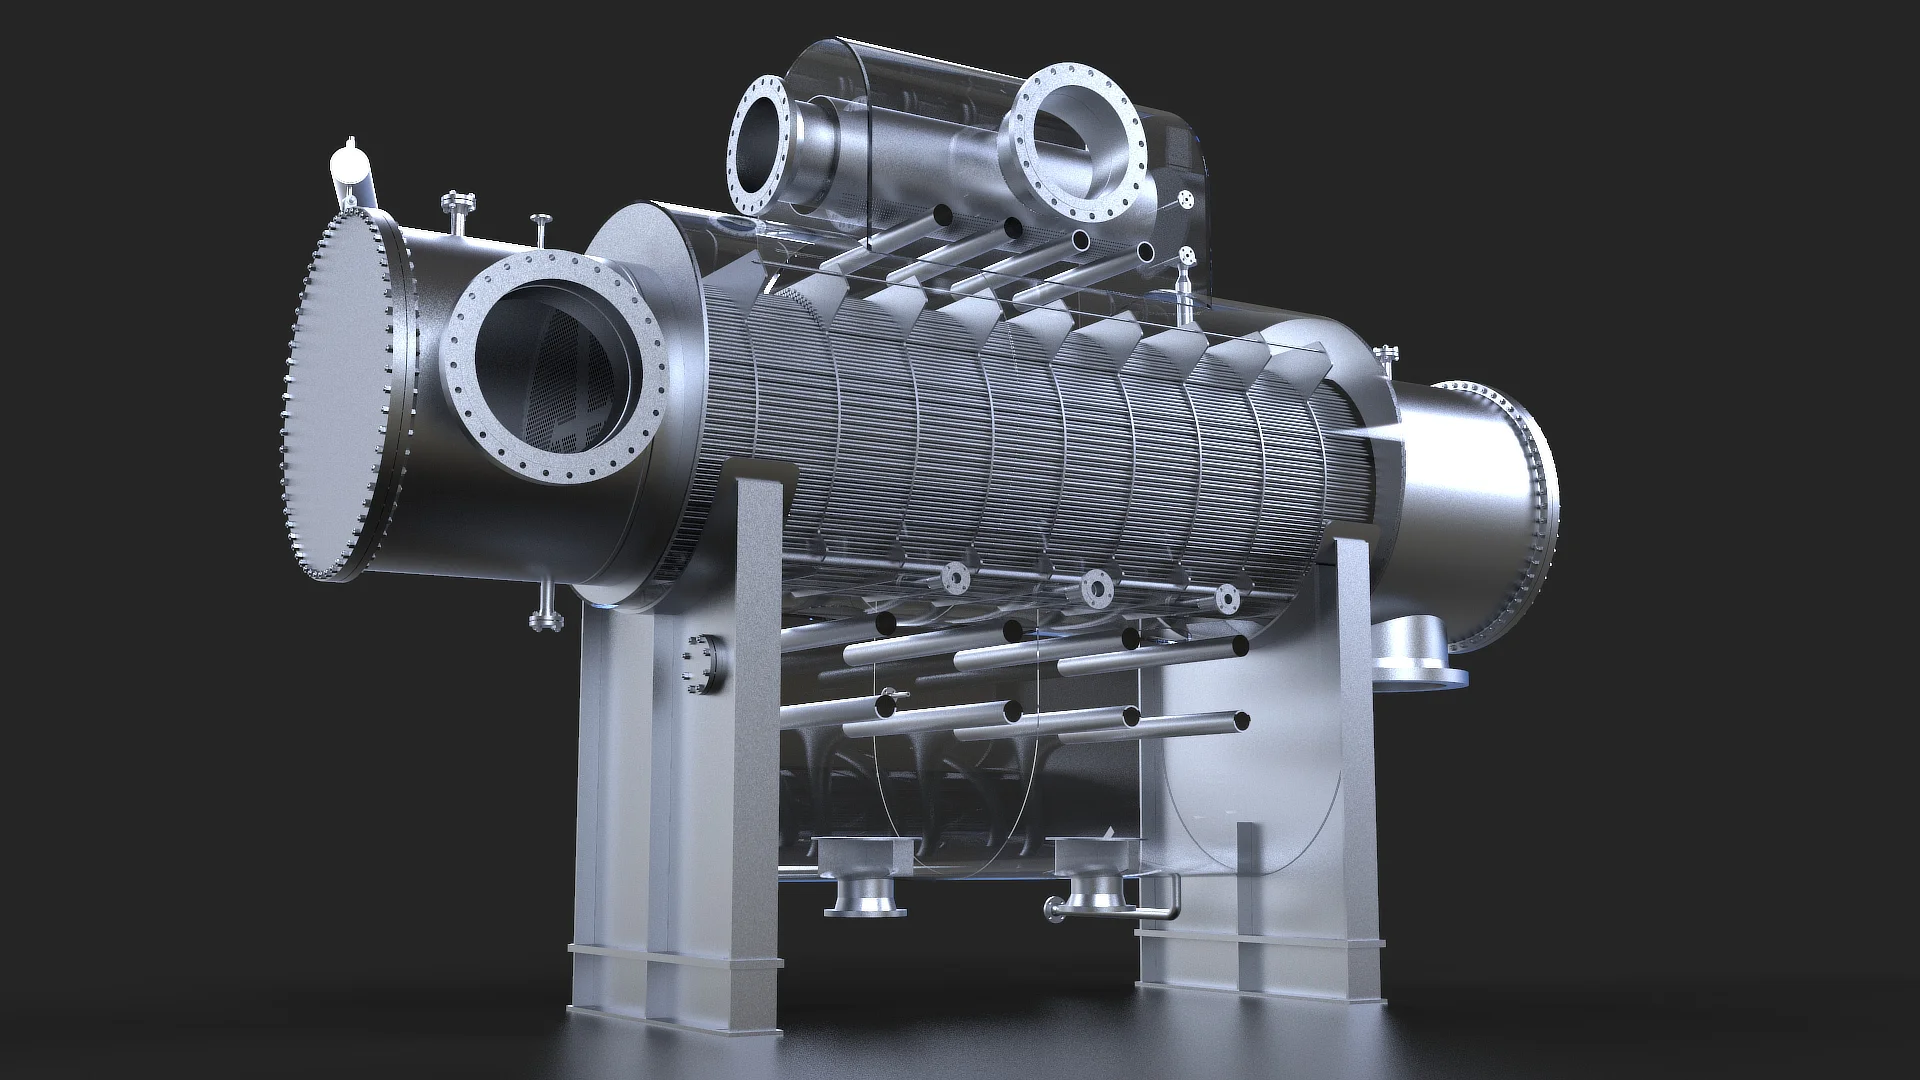
Our Shell & Tube Heat Exchangers are engineered for demanding process applications where thermal performance, mechanical integrity and long-term reliability are critical.
From conventional duties to highly complex operating conditions, we combine proven heat transfer principles with advanced engineering to deliver solutions built around the precise demands of each application.
Designed around your process.
No two applications place exactly the same demands on a heat exchanger. That’s why every solution is engineered around the specific process conditions, materials, pressures, temperatures and performance requirements involved.
From thermal and hydraulic design through to mechanical analysis and manufacture, we consider the complete operating environment to deliver equipment that performs reliably throughout its working life.
Built for demanding conditions.
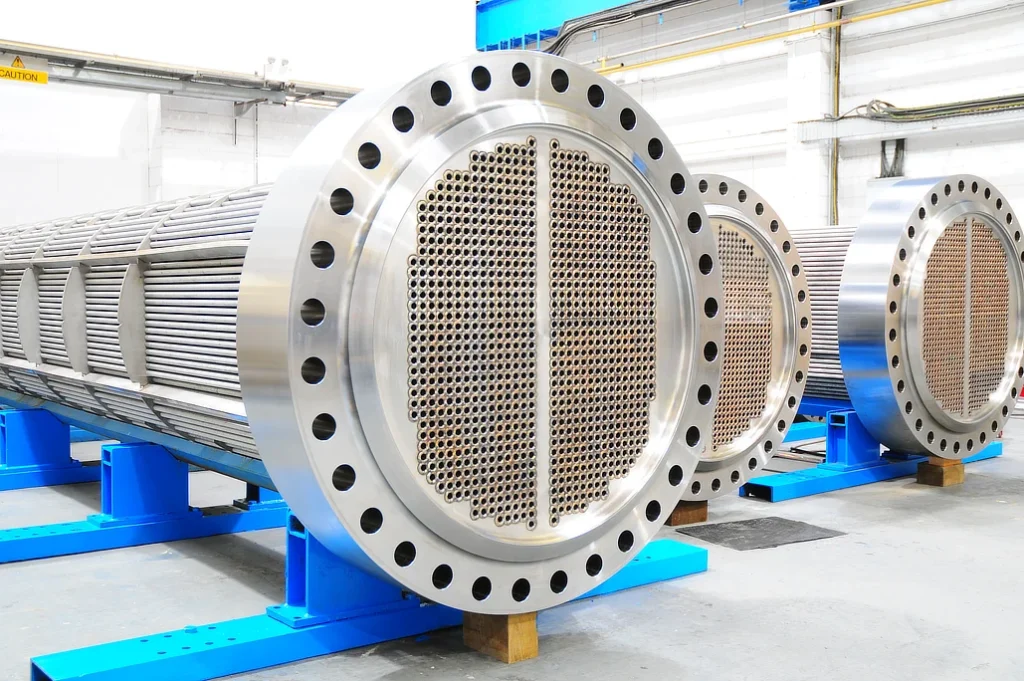
Shell and tube heat exchangers are often required to operate under extreme pressures, temperatures and corrosive conditions. Reliability has to be engineered in from the outset.
Our experience spans a wide range of demanding applications and materials, from carbon and stainless steels to titanium, duplex stainless steel and other corrosion-resistant alloys.
Engineered for integrity.
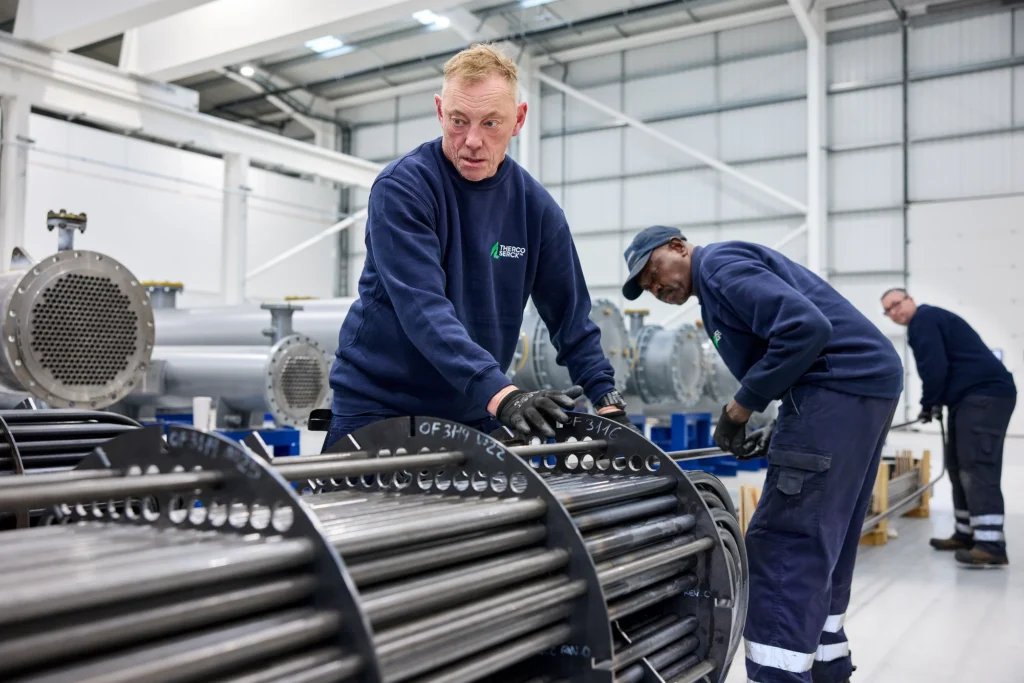
Thermal performance is only part of the equation. Our engineering approach considers thermal, hydraulic and mechanical performance together, supported where required by advanced FEA and fatigue analysis.
Every solution is designed with relevant codes, standards and client requirements built in from the beginning.
Built on experience.
Our engineers bring decades of experience designing sophisticated shell and tube equipment for critical applications across the petrochemical, oil and gas, power generation, nuclear and emerging energy sectors.
That experience helps us understand not only what needs to work on paper, but what will continue to perform in the real world.
-
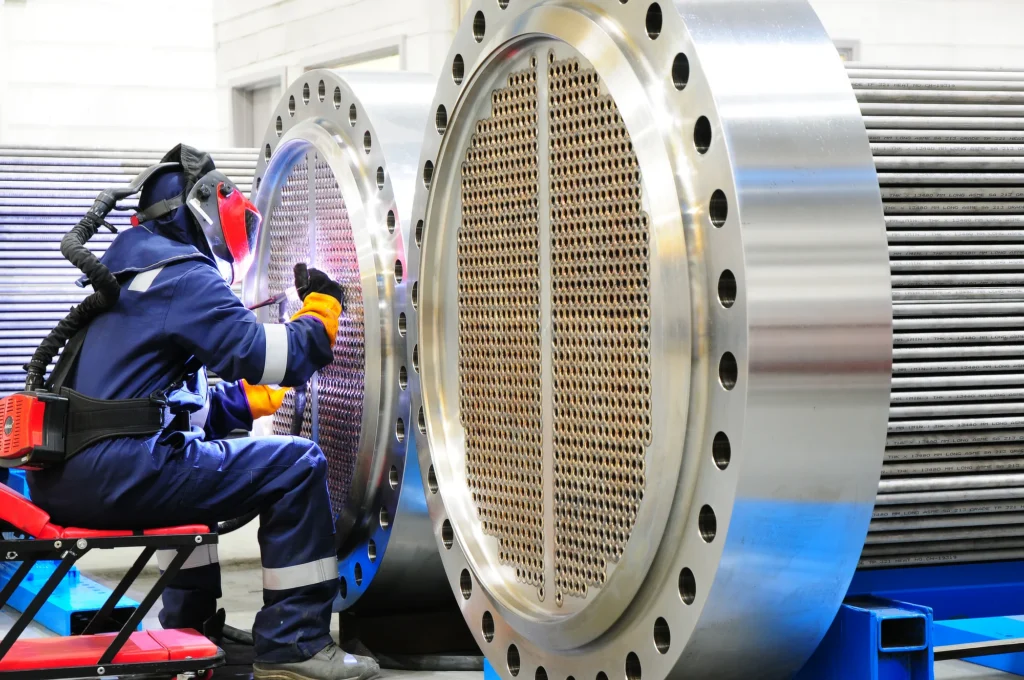
Client:
Prax Refining
Item:
Reactor Feed Effluent Exchangers
Material:
Chrome Molybdenum & Stainless Steel
Design:
ASME VIII Div 1 & TEMA ‘R’
-
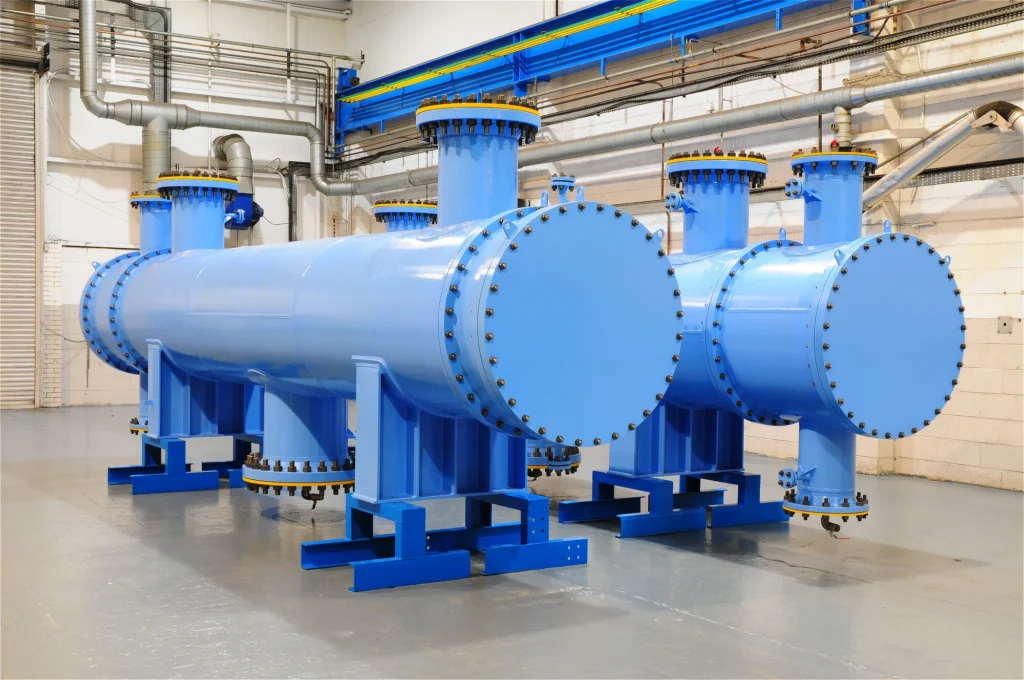
Client:
SABIC
Item:
Propylene Refrigerant Desuperheaters
Material:
Duplex Stainless & Low Temp Carbon Steel
Design:
PD5500 Cat 2, TEMA ‘R’ & Pressure Equipment Safety Regulation’s
-
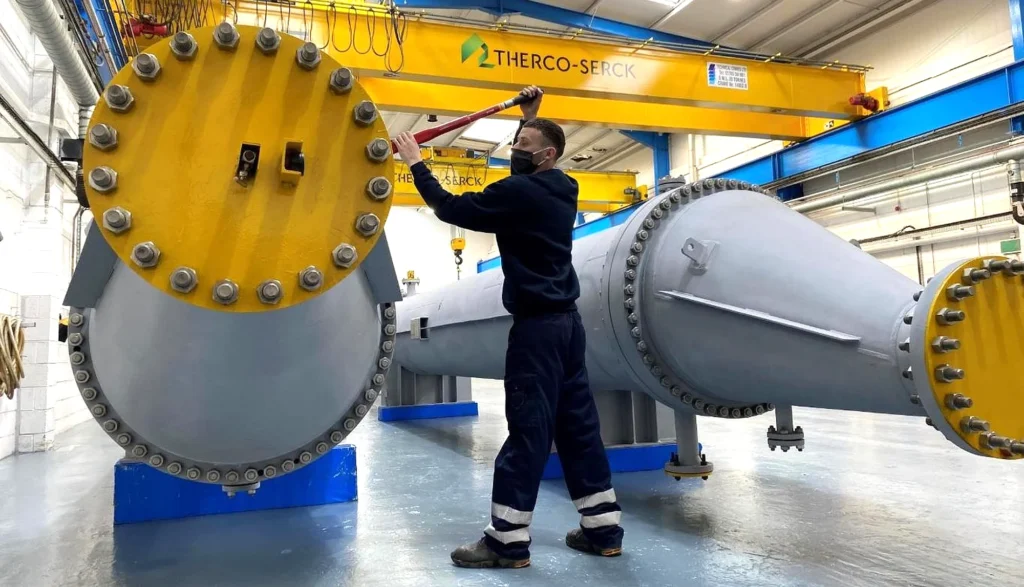
Client:
Hydrostor
Item:
Compressor Inter/After Coolers
Material:
Stainless Steel
Design:
ASME VIII Div 1 [‘U’ Stamped], TEMA ‘R’ & AS1210
-
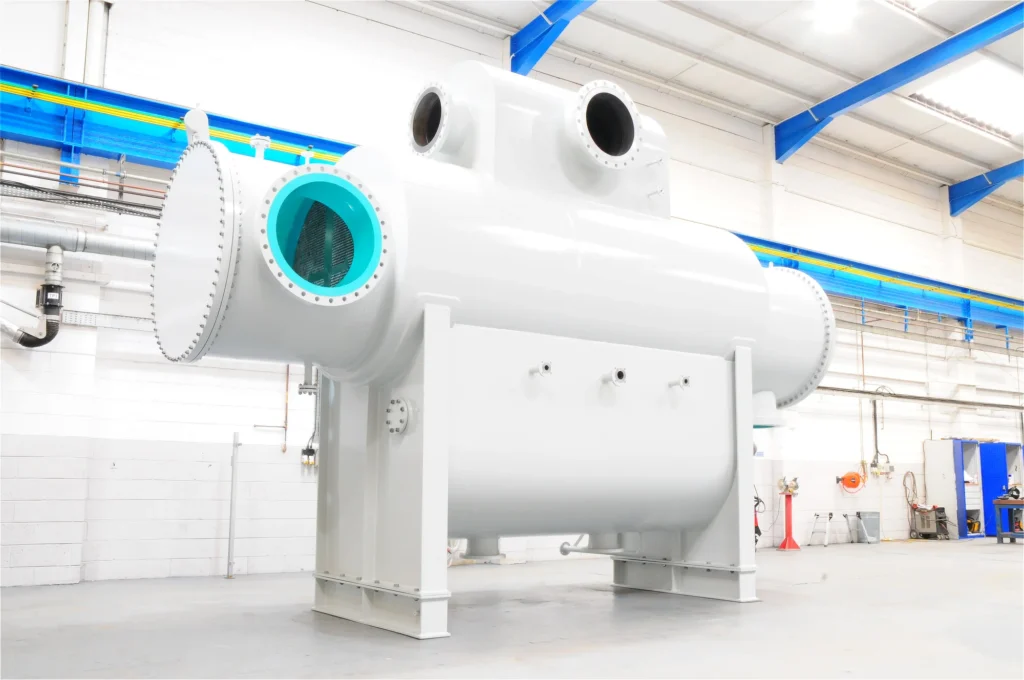
Client:
NW Total
Item:
Turbine Steal Dump Condenser
Material:
Titanium & Carbon Steel
Design:
ASME VIII Div 1, HEI ASME VIII Div 1, HEI & Pressure Equipment Safety Regulation’s
-
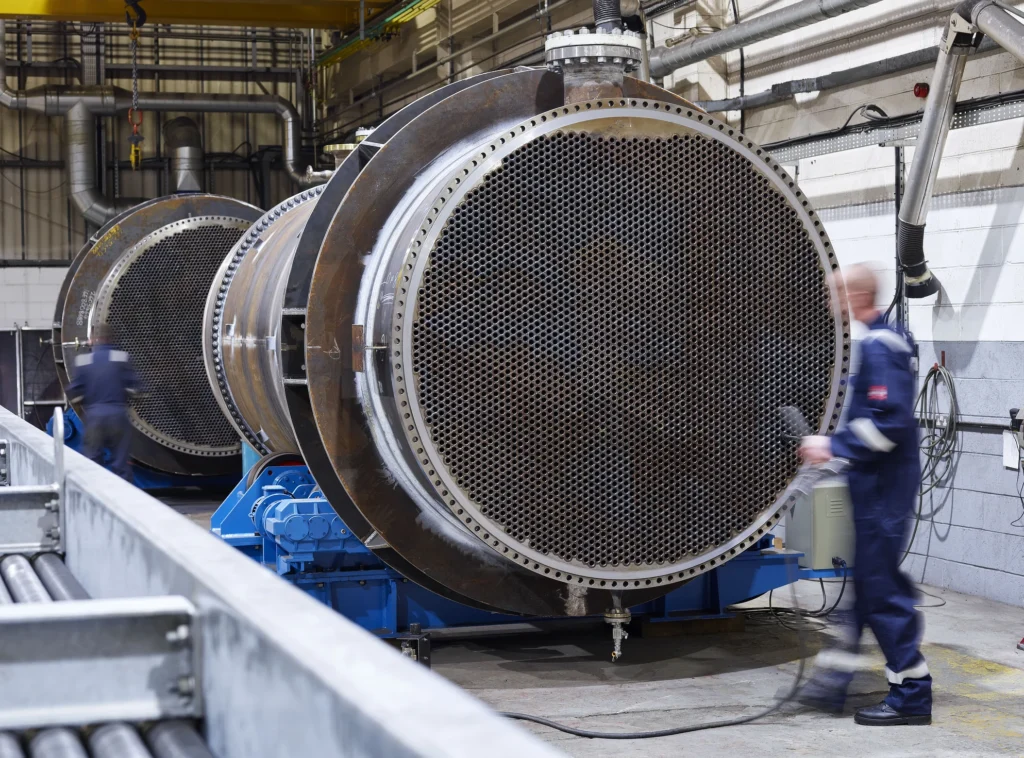
Client:
SABIC
Item:
Thermosiphon Reboilers
Material:
Carbon Steel
Design:
ASME VIII Div 1 & TEMA ‘R’
-
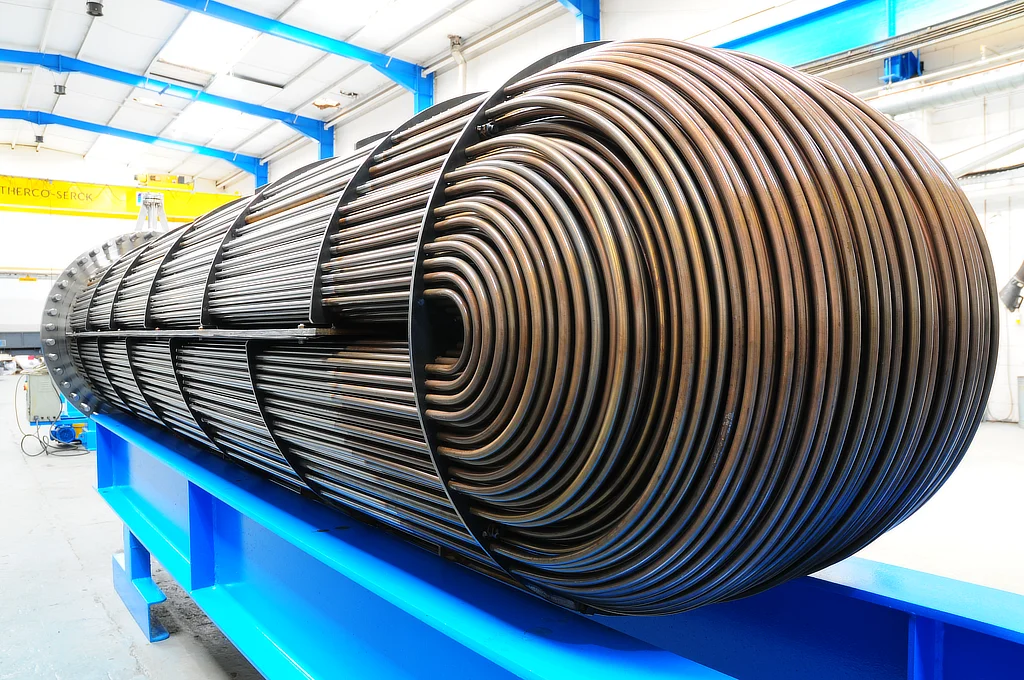
Client:
EDF Nuclear Energy
Item:
Gas Cooler
Material:
Stainless Steel
Design:
PD5500 Cat 1 & TEMA ‘R’
-

Client:
Valero Energy
Item:
HF Acid Coolers [with Rod Baffle]
Material:
Carbon Steel
Design:
ASME VIII Div 1 & TEMA ‘R’
Work with a team that understands the detail
We collaborate closely to solve problems properly, with clarity, precision and accountability at every stage.